Heating Needs In A Chemical Plant
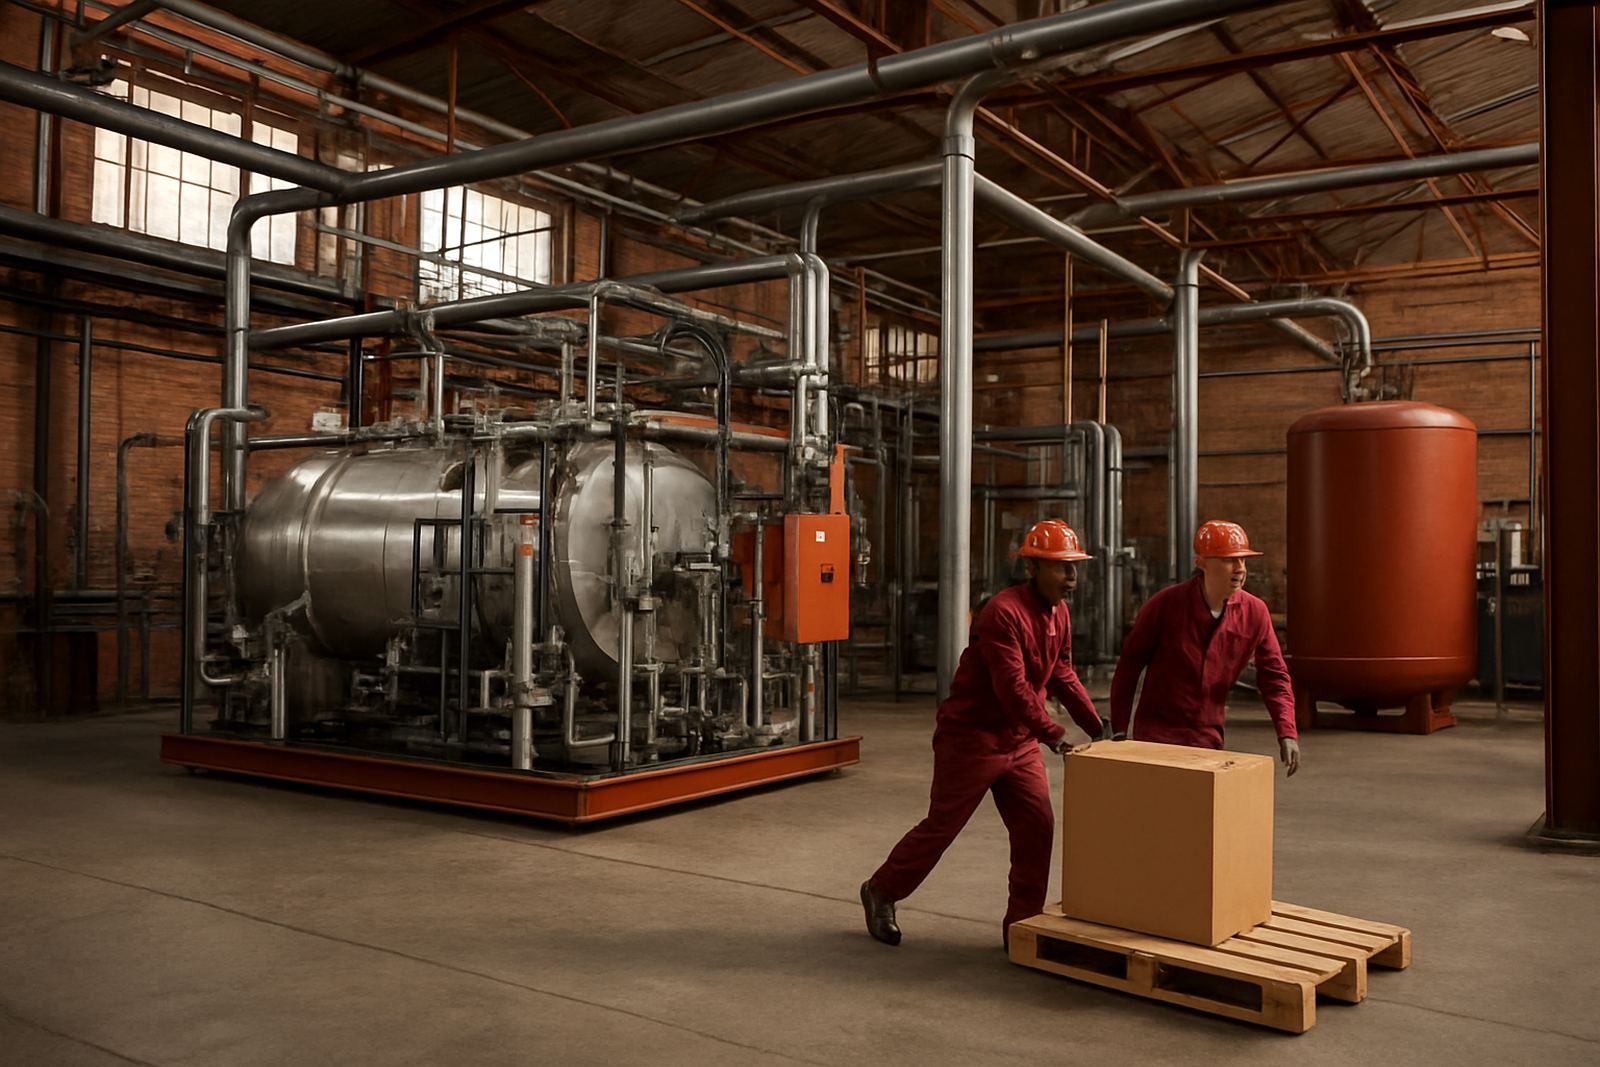
In a chemical plant, heating is rarely just about getting a vessel warm. It is about holding a setpoint, protecting product quality, avoiding overheating and keeping operators clear of unnecessary risk. The usual pain points are cold starts after load-shedding, variable feed water quality, steam losses, corrosion from humidity on the coast, and poor control on older plant that has grown in sections over the years.
We work with process teams that need dependable heat for tanks, transfer lines, wash systems, service water and plant utilities. That can mean a boiler room feeding a central steam network, or a smaller package for one process area where space is tight and shutdown time is limited. On sites around Gauteng, the biggest issue is often not the heat source itself, but the piping, controls and maintenance around it.
Typical Equipment Used On Site
A chemical plant heating package can include one or more of the following, depending on the process, temperature range and duty cycle.
- Commercial or industrial boilers for steam and hot water generation
- Calorifiers for controlled domestic or process wash water
- Inline heaters for circulation loops and small-bore process lines
- Incinerators where regulated waste handling forms part of the operation
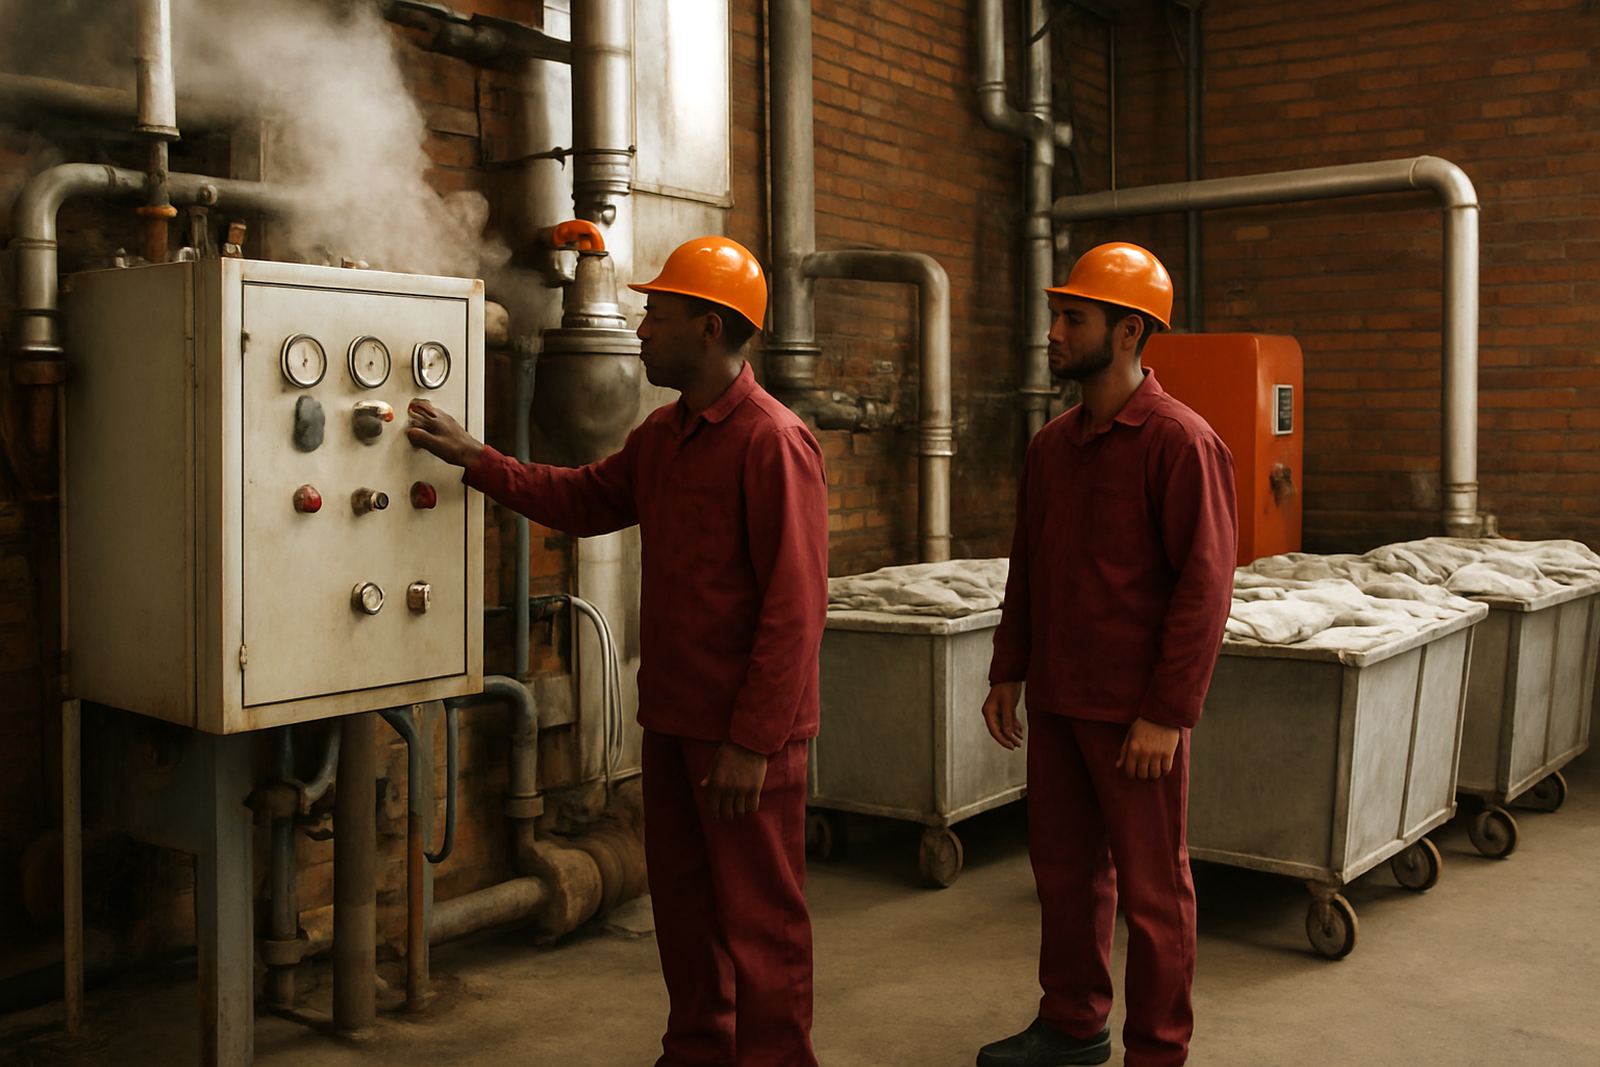
- Burners, pumps, valves, strainers, controls and safety interlocks
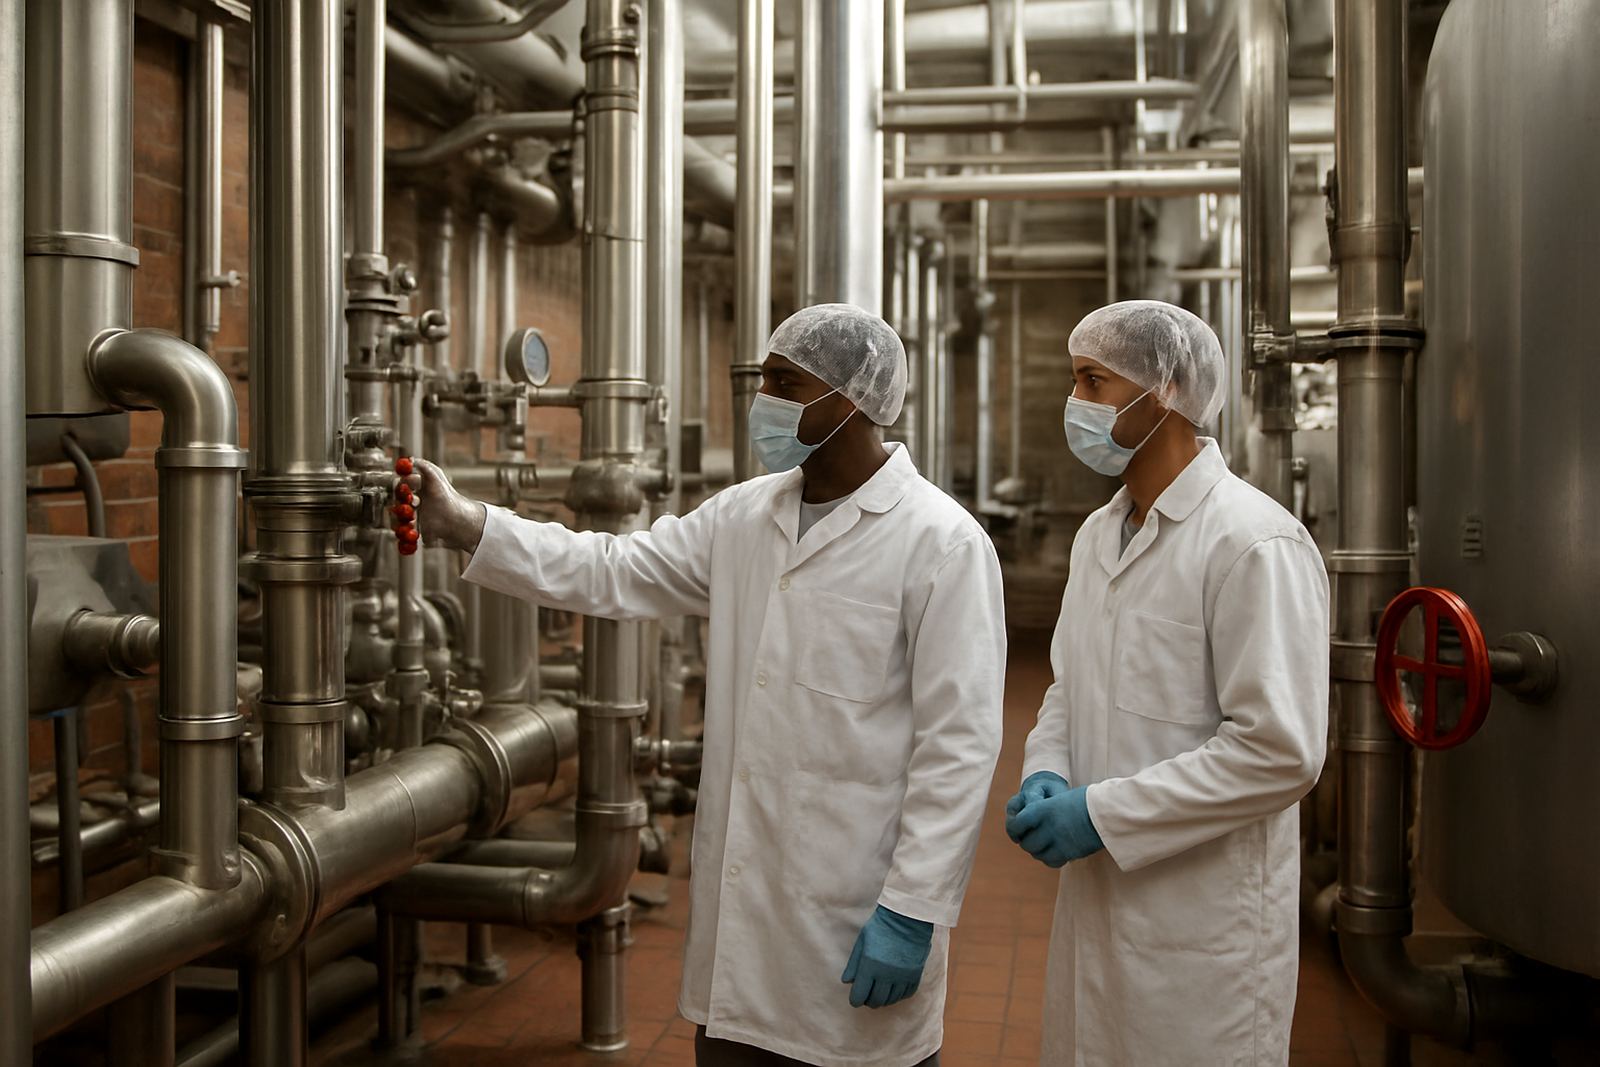
- Water treatment equipment to reduce scale, carryover and corrosion
For many plants, the right answer is a mixed system. A main boiler may carry the heavier load, while an inline heater supports a specific line or tank bay. That gives better control and helps avoid heating the whole site when only one area needs attention.
How We Plan The Layout
Good layout planning starts with the process map, not with the plant room. We look at what must be heated, the target temperature, how fast the heat is required, where the pipe runs are, and how the plant will be isolated for service. If the equipment sits too far from the user point, the system wastes energy and response time gets slow. If access is cramped, maintenance becomes expensive because every service needs extra labour and downtime.
On chemical sites, we also check safe access for operators, ventilation, drainage, fire separation and the route for flue gases. Condensate handling, expansion allowance and pipe support matter more than many teams expect. In older buildings, we often find undersized plant rooms, weak electrical supply, or pipework that was added later without proper load checks. Those jobs normally need a staged approach rather than a full stop-and-replace.
- Keep the heat source close enough to cut losses, but not in a high-traffic process zone
- Allow space for tube cleaning, burner access and valve replacement
- Plan for isolation so one line can be worked on while the rest of the plant stays running
- Check whether the site needs backup for load-shedding or after-hours production
Common Mistakes We See
One of the most common mistakes is sizing the system for peak demand only, then expecting stable control at low production. That usually causes short cycling, poor fuel use and too much wear on the burner train. Another issue is skimping on water treatment. In a chemical plant, scale inside a boiler or calorifier can cut heat transfer fast, and then operators start turning up the firing rate to compensate, which pushes costs even higher.
We also see plants where the controls are not matched to the process. A simple on-off arrangement may be fine for one utility duty, but not for a line that needs fine temperature control through winter mornings. Poor maintenance planning is another problem. If a site waits for a failure before booking service, it often ends up paying for emergency callouts, lost production and rushed parts. That is not a good position when a batch schedule is already tight.
Maintenance That Keeps Production Moving
Our service teams handle boiler servicing, calorifier maintenance, inline heater repairs, incinerator servicing, annual inspections, combustion tuning, refractory relining and water treatment support. For plants in Gauteng, we can reach Boksburg, Germiston, Kempton Park, Midrand, Sandton and Pretoria quickly, and we support sites nationally where shutdown windows are planned in advance.
For chemical plants, the practical aim is simple: keep heat available, keep fuel use under control, and catch wear before it becomes a safety issue. That means checking burners, cleaning heat transfer surfaces, testing safety controls, looking at pump condition, and reviewing water quality records. If there has been a pressure drop, uneven heat, burner lockout or excessive stack temperature, we trace the cause and not just the symptom.
- Seasonal checks before winter and before major production runs
- Emergency callouts for lockouts, low water issues and failed controls
- Planned shutdown work to avoid overtime and rushed repairs
- Refurbishment work when older plant still has life left in it
Budget Ranges For Chemical Plant Heating
Budget depends on duty, capacity, materials and how much existing plant can be reused. A smaller inline heater repair or control fault on a utility loop may sit in the tens of thousands of Rand. A full boiler service with combustion tuning and safety checks often falls into a mid-range service budget, while a plant refurbishment with pipework changes, controls upgrades and refractory work can run into a much larger capital spend.
As a working guide, many chemical plant clients start with service and fault-finding budgets from about R8 500 to R35 000 for smaller jobs, R35 000 to R120 000 for more involved maintenance or partial upgrades, and from about R150 000 upwards for new heating packages or significant refurbishment. The final number depends on site access, materials, shutdown timing and whether fabrication is needed in our Jet Park workshop or on site. We prefer to price it clearly before work starts, so the maintenance team and accounts team are not left guessing later on.
Why Chemical Plants Use Ai-TEC
Ai-TEC has been working with boiler and process heating systems since 2009, with a Boksburg base and service teams that support Gauteng and the rest of South Africa. Our team includes an MD, project engineering, operations, service coordination, fabrication and boiler technical support, so jobs are handled from first call through to commissioning and follow-up. That matters on chemical sites where a quick repair is not enough unless the system is also set up to stay stable afterwards.
We work with practical plant constraints: load-shedding, limited shutdown windows, coastal humidity, municipal water quality and safety paperwork. If your tanks, lines or utility systems need controlled heating, we can assess the site, recommend the right package and support it with planned maintenance. Send the details to engineering@ai-tec.co.za and we will respond with the next steps.