What a steam trap actually does in a live plant
The purpose of a steam trap is simple: pass water and air out of the line without losing usable steam. In practice that means it sits between the steam side and the condensate side, opening when condensate builds up and closing when hot steam reaches it. If it works properly, coils heat evenly, radiators or process equipment respond faster, and the boiler does not have to keep chasing lost heat.
When a trap fails open, live steam escapes straight into the condensate return or drain. When it fails closed, water backs up in the line and the system starts hammering, underheating or flooding. Both faults cost money, and both are common on plants that run long hours or get little attention between shutdowns.
How failure shows up on the ground
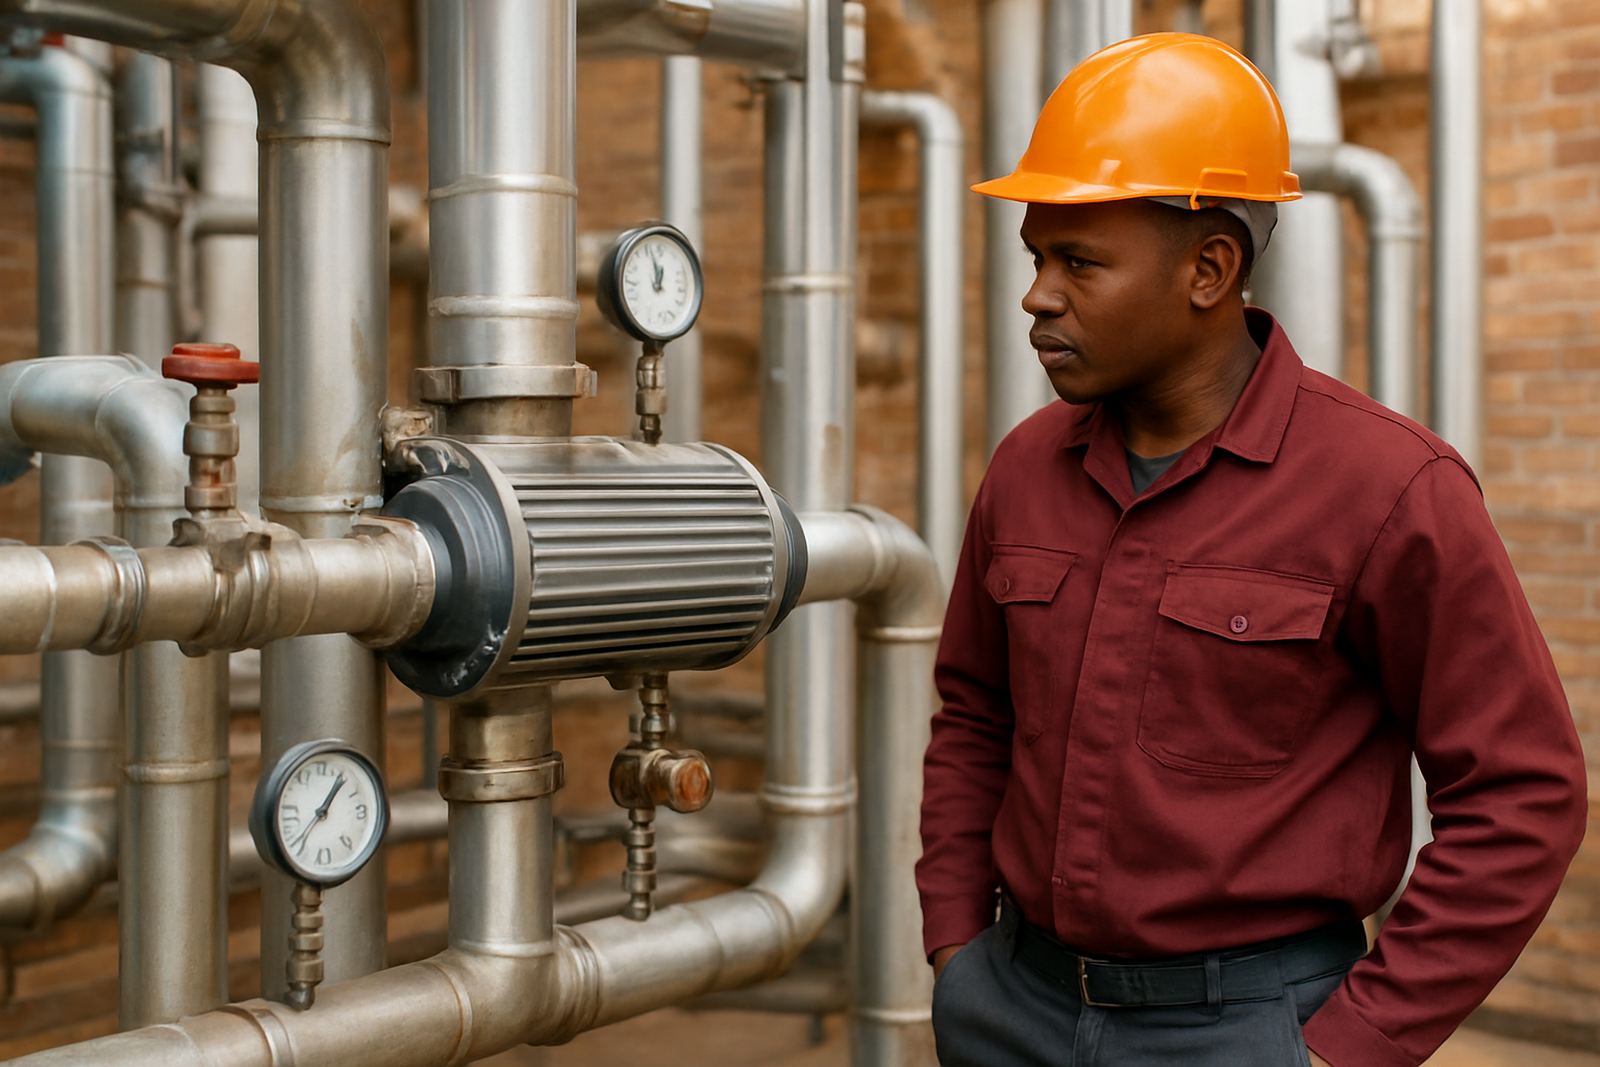
Most trap faults do not start with a dramatic breakdown. They usually show up as small changes in temperature, noise or fuel use. A section that used to heat evenly starts to lag. A return line gets hotter than it should. Someone hears water hammer after start-up, then leaves it until the next breakdown. In many Gauteng factories, that delay carries on for months.
- Cold spots on heaters, calorifiers or process coils
- Wet steam and poor condensate drainage
- Water hammer in the pipework
- Higher gas, diesel or coal use for the same output
- Extra strain on valves, joints and gaskets
There is also the hidden cost of downtime. If a steam trap on a wash line, food plant or laundry fails, the issue is not only heat loss. It can affect output quality, shift targets and maintenance callouts as well.
Why failed traps waste so much energy
Steam contains a lot of usable energy, so every leak matters. A trap that passes steam is not just losing vapour, it is losing the heat that the boiler paid to create. That means the boiler fires longer, the burner cycles more often, and the plant uses more water treatment, more fuel and more make-up water than planned.
On a busy site in Boksburg or Kempton Park, this can be hard to notice because production keeps going. But over a month the effect adds up. One failed trap can keep a small coil warm enough to fool operators while steadily bleeding energy. A group of failed traps can make a well-run boiler room look inefficient even when the boiler itself is in good condition.
Condensate also matters. If traps do not discharge properly, condensate stays in the system and blocks steam flow. That slows heat transfer and can cause corrosion, especially where the plant sees shut-downs over weekends or load-shedding interruptions. In coastal air the issue can be worse, but even inland humidity and poor insulation will shorten component life.
A local example from a Gauteng plant
We recently saw a medium-sized plant near Germiston with intermittent heating on a process line. The operator had already checked the boiler and pressure controls, but the line still took too long to come up to temperature. During a trap survey, several traps were found passing steam, while two others were blocked with dirt and scale. Once those units were replaced and the line was flushed, the heat-up time dropped and the boiler stopped working against itself.
That kind of fault is common where water treatment is not being kept up, or where traps have not been checked since the last shutdown. It is also common after contractors leave the site and nobody includes trap checks in the monthly maintenance round. The plant had been spending money on energy while the real problem was sitting at line level.
For older systems, we often find that the issue is not one bad trap but a pattern of wear. A few traps fail open, others fail shut, and the result is an uneven system that is hard to control.
What to check before the next breakdown
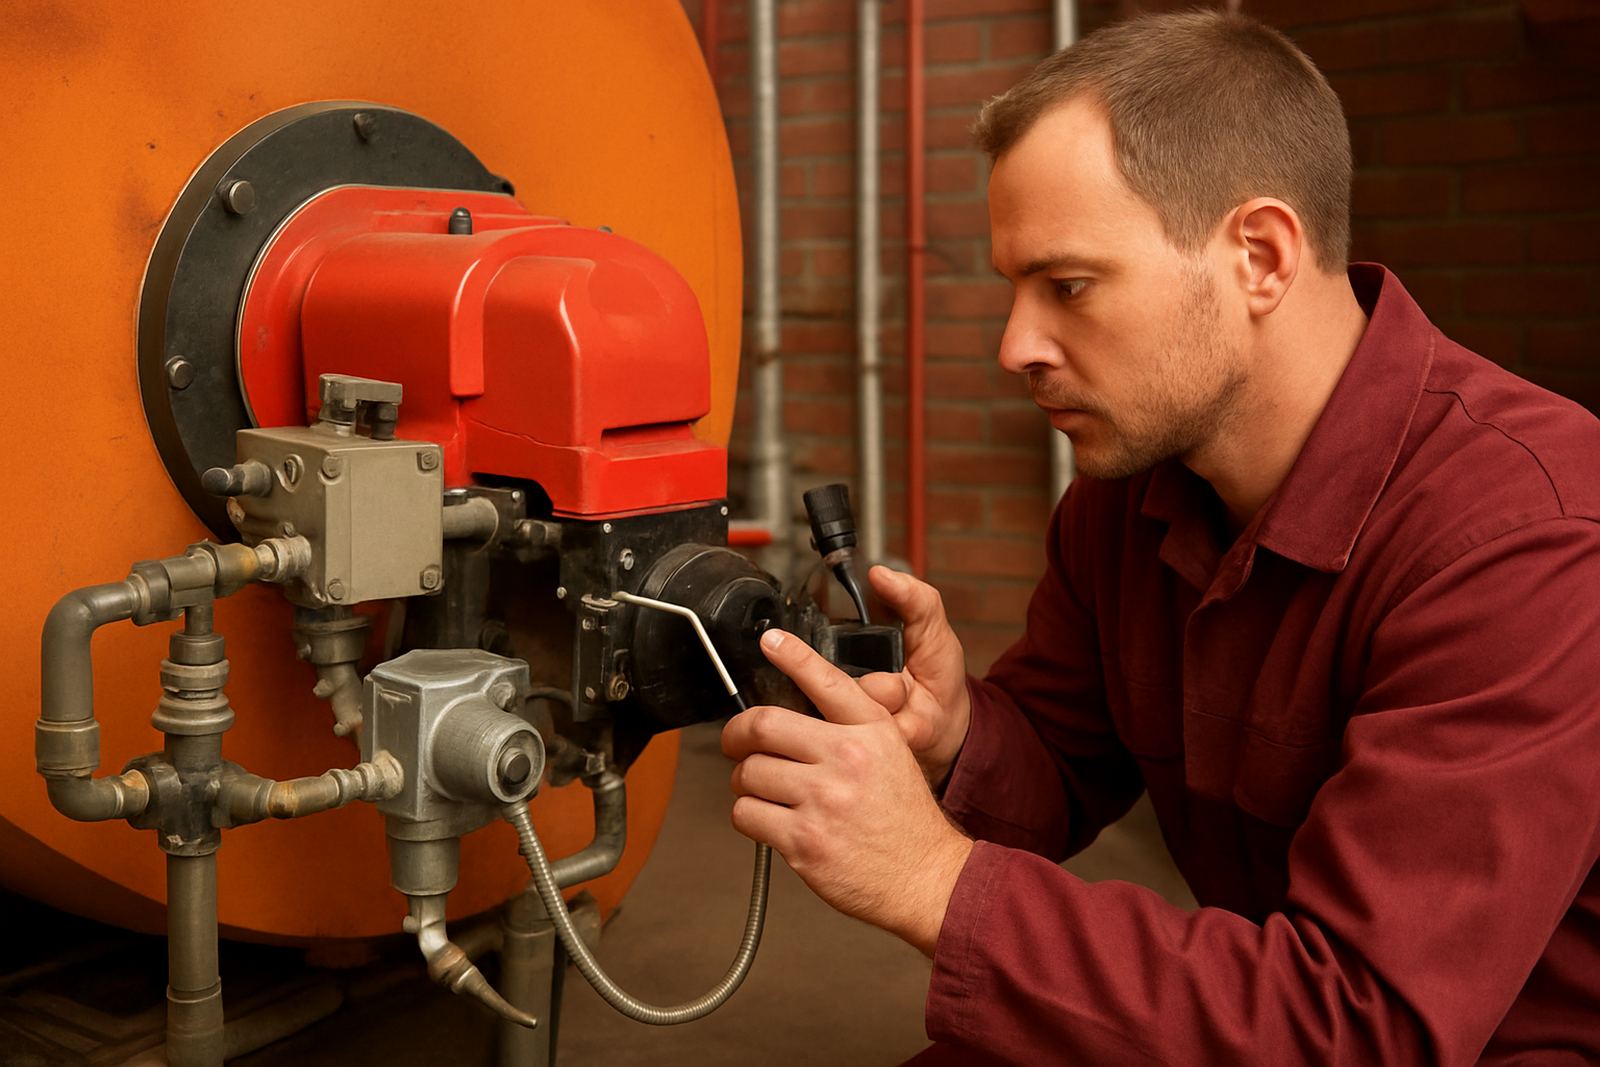
Steam trap inspections should be part of routine boiler and plant maintenance, not only a response to a fault. A proper check looks at temperature, discharge pattern, isolation valves, strainers and the condition of the return line. It also tests whether the trap type still suits the duty. Some traps cope better with start-up air, others handle dirty condensate better, so the right fit matters.
- Check traps during normal operating temperature, not only when the plant is cold
- Record each trap location, duty and last service date
- Inspect strainers and upstream valves at the same time
- Look for signs of flashing, hammering or back pressure
- Match the trap to the load, pressure and condensate volume
It helps to link trap checks to annual inspections and boiler servicing. That way faults are caught before they affect the entire line. On sites with shutdown windows, this is also the best time to replace worn parts without disrupting shifts.
Keeping steam traps useful, not expensive
The real purpose of a steam trap is not only to remove condensate. It is to keep a steam system controllable, safe and efficient. When traps are maintained properly, the boiler room runs steadier, the plant uses less fuel, and operators spend less time fighting faults that should have been prevented.
For sites in Gauteng and beyond, the best results come from planned maintenance, water treatment support and prompt repairs when a trap starts failing. If a heating line, calorifier bank or process system is underperforming, the traps are worth checking before bigger parts are replaced. Many expensive problems start with a small unit that was left out of the maintenance plan.
At Ai-TEC, we service commercial and industrial heating systems from our Jet Park base and support sites nationally. For steam trap checks, boiler maintenance or plant refurbishment planning, contact engineering@ai-tec.co.za.